

Multi-Functional Safety Gate Valve: High-Pressure Manifold Flow Isolation
Controlling high-pressure fluid streams across surface standpipe manifolds, pump discharge lines, and well test spreads requires robust, multi-functional flow isolation hardware. Standard manifold valves often lack the versatility required to handle rapid pressure shifts, bidirectional sealing demands, and emergency shut-in protocols simultaneously. To provide uncompromised surface flow control and enhanced safety compliance, modern drilling sites deploy the Multi-Functional Safety Gate Valve. Engineered with an advanced slab-gate architecture, pressure-energized seats, and rapid actuation capabilities, this specialized valve ensures absolute fluid isolation and operational flexibility across all surface manifold configurations.
1. The Advanced Engineering Architecture of Manifold Isolation
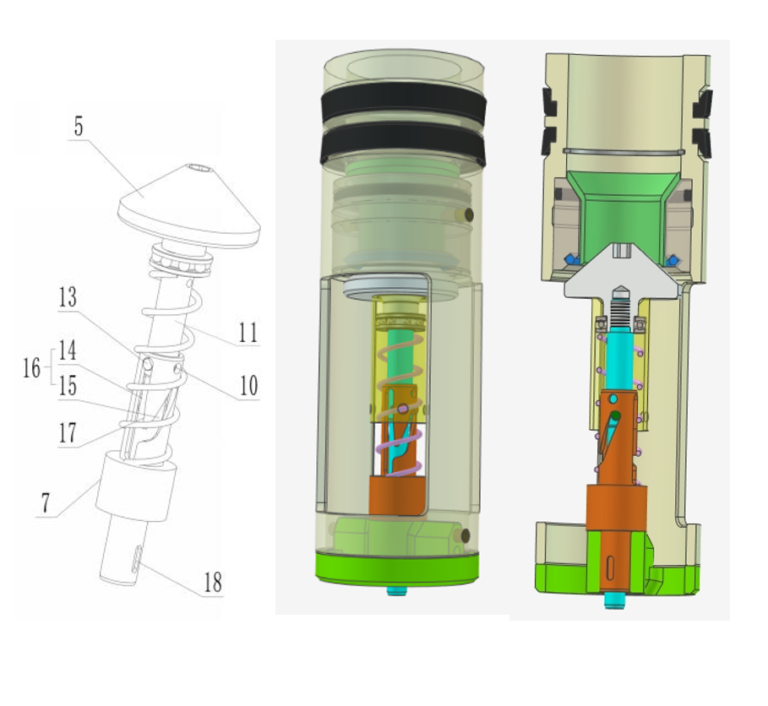
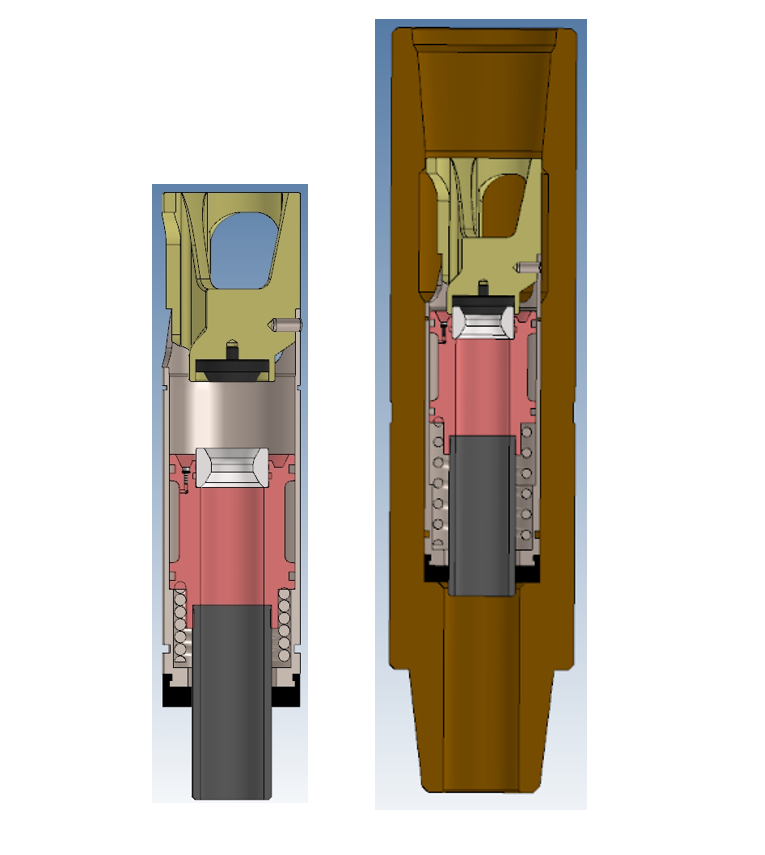
Unlike conventional single-purpose valves, the multi-functional safety gate valve is engineered to integrate multiple operational requirements into a single compact housing.
- Bi-Directional Floating Seat Design: Utilizes spring-loaded and pressure-energized seat rings that maintain continuous contact with the flat slab gate, guaranteeing absolute bubble-tight sealing from either flow direction.
- Low-Torque Multi-Start Stem Assembly: Precision-machined stem threads and low-friction thrust bearings enable rapid manual handwheel operation or seamless integration with hydraulic actuators under maximum working pressures.
- Full-Bore Unobstructed Flow Path: Designed with an identical inner diameter to the mating piping, eliminating flow turbulence, pressure drops, and localized erosive scouring across the valve cavity.
2. Key Operational Advantages and Performance Metrics
- Versatile Manifold Integration: Easily adapts to standpipe manifolds, choke and kill lines, cement units, and fracturing spreads, reducing inventory complexity while maximizing safety.
- Rapid Emergency Shut-Off: Provides instant, positive closure during unexpected pressure spikes or surface equipment failures, safeguarding personnel and protecting downstream infrastructure.
- Extended Service Life Under Abrasive Conditions: Engineered to withstand abrasive drilling muds, cement slurries, and high-pressure well test fluids without degradation of sealing integrity.
3. Engineering for Harsh Surface Environments
- Tungsten-Carbide and Stellite Armored Sealing Faces: Critical gate edges and seat faces are heavily hardfaced with cobalt-base alloys or tungsten carbide to resist severe high-velocity fluid cutting.
- API 6A and NACE Compliant Forgings: Forged from high-grade alloy steels designed to withstand intense cyclic pressure shocks, mechanical stress, and aggressive sour gas ($\text{H}_2\text{S}$) environments.
4. Conclusion
Surface safety and manifold reliability are non-negotiable in modern drilling and well servicing. By combining bi-directional slab-gate mechanics with rugged erosion-resistant armoring, the Multi-Functional Safety Gate Valve guarantees absolute flow isolation and operational confidence under the most punishing pressure loads.